

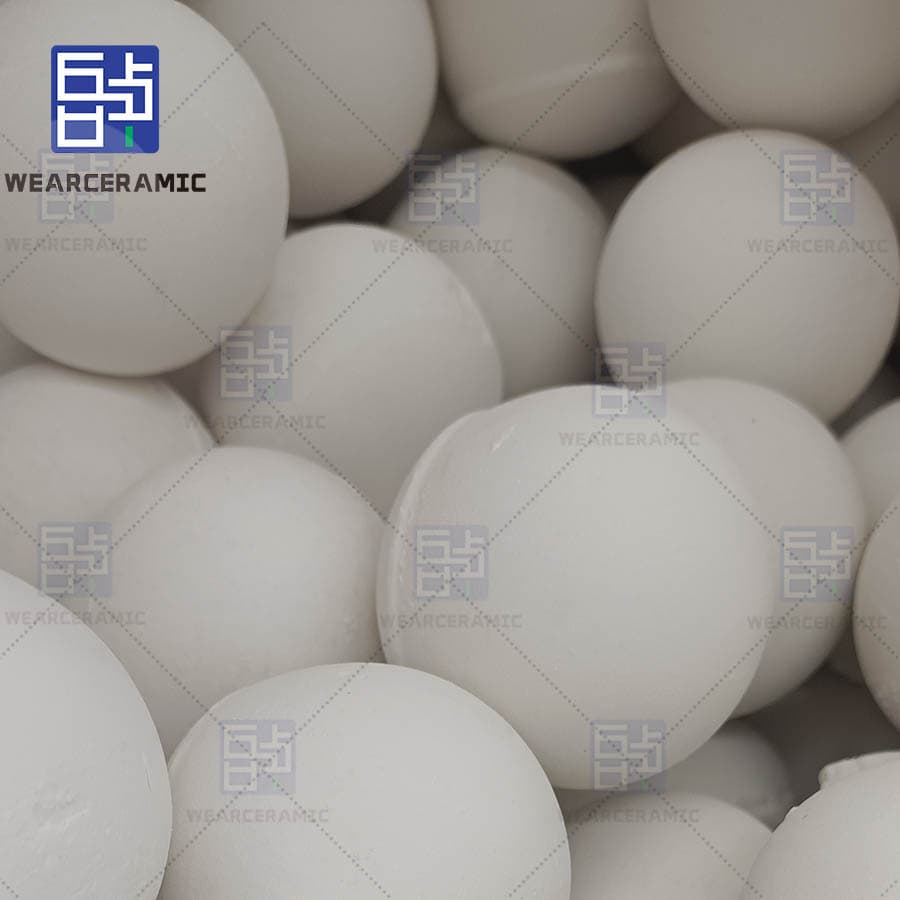
70% Alumina Content 50 mm Ceramic Packing Ball
Reduce Shutdown Costs with Reliable Alumina Inert Ceramic Balls
Built for Long Service Intervals
Industrial reactors are expected to run continuously for months or even years before scheduled maintenance. During this period, support media must withstand constant load, pressure fluctuations, temperature changes, and process media exposure.
The 50 mm alumina ceramic balls are designed to maintain structural integrity throughout these extended operating periods. Their optimized alumina composition provides the mechanical strength required for supporting heavy catalyst beds while remaining economically attractive for large-volume installations.
Instead of focusing solely on initial material cost, many plant operators evaluate total lifecycle performance. Longer service life often translates directly into reduced maintenance expenditure.
Supporting Process Stability
A catalyst can only perform efficiently when process flow remains stable.
Uniformly manufactured ceramic balls help create a balanced support layer that promotes even distribution of gases and liquids throughout the reactor. This reduces the risk of localized channeling, uneven catalyst utilization, and pressure-drop irregularities.
The result is a more predictable operating environment that supports consistent production quality over time.
Common Industries Benefiting from Alumina Support Media
Oil Refining Facilities
Used in hydroprocessing, desulfurization, reforming, and other reactor systems requiring dependable catalyst support.
Renewable Fuel Production
Increasing numbers of biofuel and renewable diesel projects utilize inert ceramic media within processing equipment to protect catalyst systems and improve operational reliability.
Industrial Gas Treatment
Widely applied in units handling process gases where temperature resistance and mechanical durability are essential.
Chemical Manufacturing Plants
Suitable for reactors processing acids, alkalis, and various chemical intermediates.
Designed for Large-Scale Industrial Projects
Large projects often require thousands of kilograms of support media delivered on schedule.
Our production capability allows us to supply bulk quantities while maintaining consistent dimensional accuracy and physical properties. This helps engineering contractors and plant operators avoid installation issues caused by mixed-quality materials.
Key advantages include:
Stable alumina composition
Consistent ball diameter
Excellent load-bearing capacity
Reliable thermal resistance
Low maintenance requirements
Efficient bulk supply capability
Quality Beyond Specifications
Successful reactor operation depends on more than laboratory test data.
Each production batch undergoes systematic inspection to verify dimensional consistency, crushing resistance, water absorption, and overall product integrity.
This quality-focused approach helps ensure that every shipment performs as expected once installed in the field.
Packaging for Global Delivery
Whether destined for a refinery expansion project in the Middle East, a fertilizer plant in Southeast Asia, or a chemical facility in South America, products are packed to withstand international transportation conditions.
Available packaging options include export bags, jumbo bags, and customized solutions according to project requirements.
Why Choose SHANDONG TITAN INDUSTRIAL CERAMICS CO., LTD.
Industrial buyers increasingly seek suppliers capable of providing not only products, but also dependable long-term support.
We offer:
Extensive experience in industrial ceramics
Stable production capacity
Consistent export quality
Flexible packaging solutions
Technical support before and after delivery
Fast response to project inquiries
Our goal is to help customers achieve safer, longer, and more efficient reactor operation.
CTA
Planning a catalyst replacement project or upcoming plant turnaround?
Contact SHANDONG TITAN INDUSTRIAL CERAMICS CO., LTD. to discuss your reactor requirements and receive a tailored quotation for high-performance alumina inert ceramic balls.
Hot Tags: 70% alumina content 50 mm ceramic packing ball, manufacturers, suppliers, factory, price, made in China, alumina ceramic balls, Alumina Ceramic Stuffing Balls, Alumina Support Balls, High Purity Alumina Filler Ball, Sintered Alumina Ceramic Ball, Thermal Storage Ceramic Ball
You Might Also Like


Send Inquiry